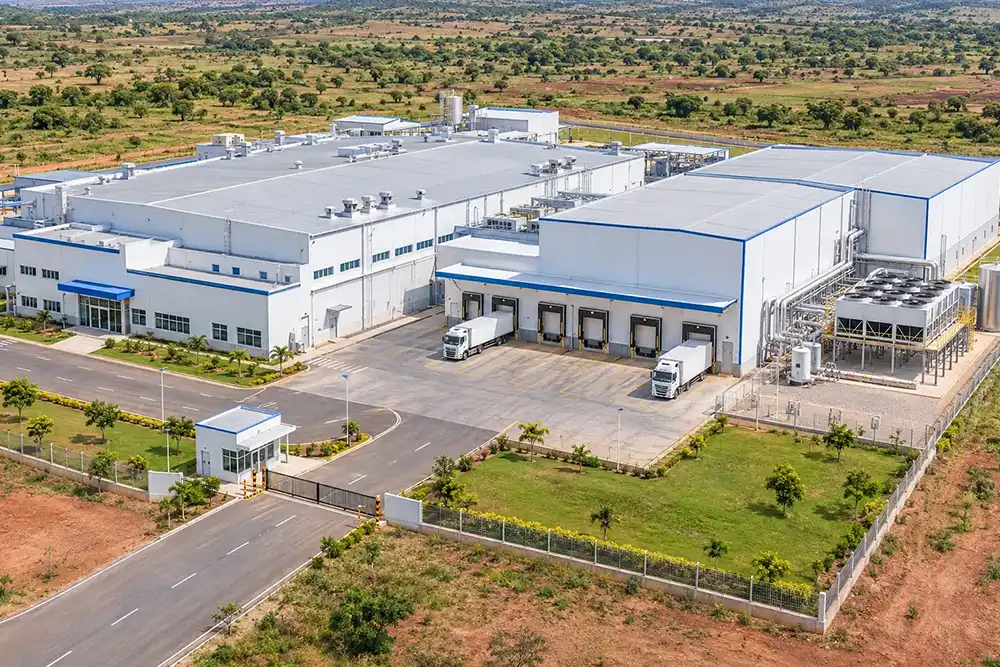
3,000 BPH Poultry Slaughterhouse Cold Storage Project in Africa
A poultry processor in Africa needed cold storage for a 3,000 BPH slaughter line, supporting continuous cutting and packing operations.
LINBLE specified three 15-ton blast freezers and two 200-ton frozen-storage rooms, accounting for high ambient temperatures, unstable power and demanding cleaning conditions.
Poultry Cold Storage Requirements
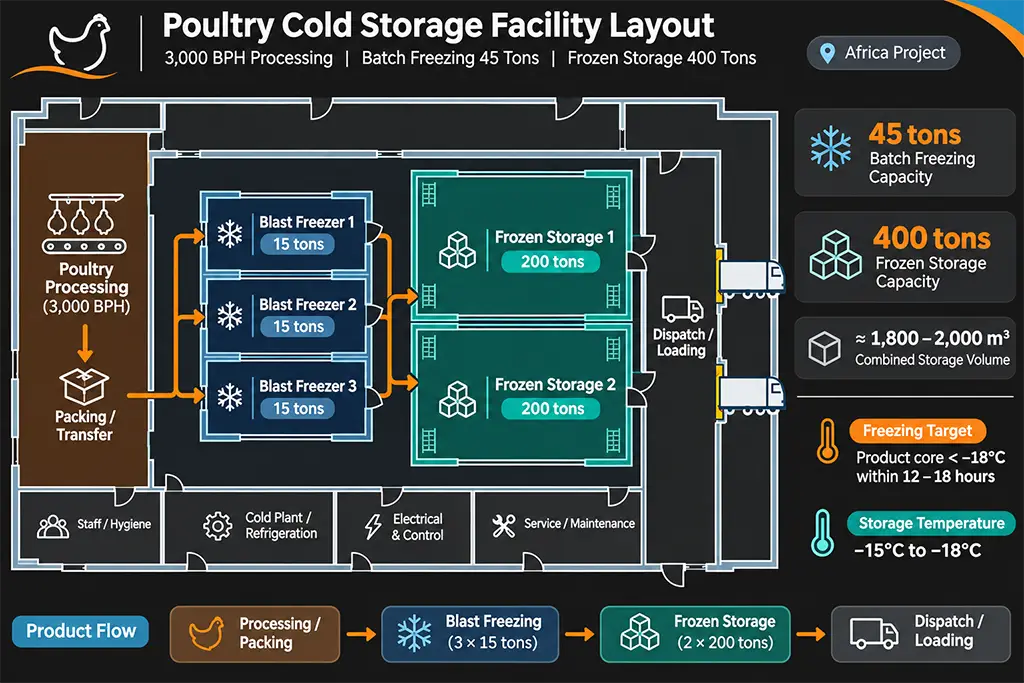
The project supported a 3,000 BPH poultry processing plant in Africa, where the customer required 45 tons of batch-freezing capacity and 400 tons of frozen storage to accommodate daily processing and distribution needs.
Project Parameters | Project Specifications |
Slaughter line | 3,000 birds/hour (BPH) |
Blast freezing rooms | 3 rooms, 15 tons nominal capacity each |
Freezing target | Product core below −18°C within 12–18 hours |
Frozen storage rooms | 2 rooms, 200 tons nominal holding capacity each |
Frozen storage design range | −15°C to −18°C, subject to confirmation of operating setpoint |
Combined storage volume | Approximately 1,800–2,000 m³ as specified |
Site Challenges & Custom Solutions
High temperatures, unstable power, repeated trolley loading and high humidity presented distinct challenges, each requiring specific refrigeration and structural measures.
01 High Temperatures & Voltage Fluctuations
Site temperatures were reported at 40–43°C, alongside voltage variations of approximately ±15% and occasional power interruptions.
These conditions affect condenser selection, compressor protection and the way equipment responds when power quality falls outside the intended range.
01 Refrigeration & Electrical Protection
To accommodate high ambient temperatures and voltage fluctuations, the refrigeration system combined heavy-duty equipment selection with dedicated electrical protection measures.
- Compressors: Bitzer screw compressor units.
- Condensers: +45°C design, 20% heat-exchange allowance.
- Voltage Protection: Overvoltage, undervoltage and phase-sequence protection.
- Controls: Discharge-temperature protection and dual-unit backup logic.
02 Airflow & Frost During Batch Freezing
Chicken portions would arrive from a high-throughput processing line rather than as one isolated daily load. Air had to circulate through loaded trolley racks, while moisture entering the room could accelerate evaporator frost accumulation and affect the freezing cycle.
02 Evaporator & Airflow Design
Each 15-ton blast freezer used a pressure-gradient air distribution arrangement to direct cold air through loaded poultry trolleys and reduce premature evaporator blockage.
- Air Distribution: Stepped-pressure ducts, up to 35 m throw.
- Evaporators: High-air-volume units with variable fin spacing.
- Fin Spacing: 16 mm inlet, 8 mm outlet.
- Materials: Grooved copper tubes, hydrophilic-coated aluminium fins.
03 High Humidity & Frequent Cleaning
The processing environment was described as exceeding 90% relative humidity. Frequent washing and exposure to processing residues placed particular demands on panel joints, coated surfaces and door openings, where corrosion or ice buildup can complicate upkeep.
03 Insulated Panels & Door Protection
The enclosure specification addressed persistent humidity, frequent washdowns and icing around door openings through reinforced panel surfaces and heated door seals.
- Insulation: Flame-retardant PU, ≥42 kg/m³ density.
- Zinc Coating: ≥180 g/m².
- Surface Finish: Food-grade coating, thickness greater than 18 μm.
- Doors: Insulated sliding doors with 360° perimeter heating.
Installation & Commissioning
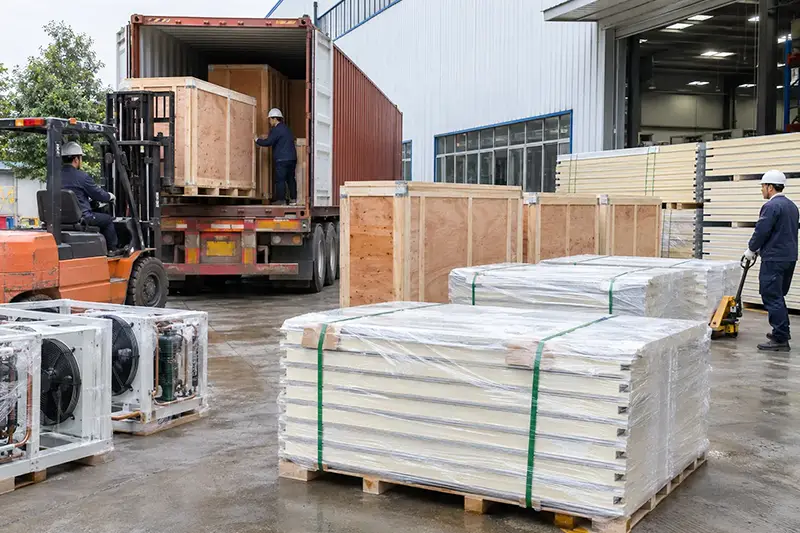
The cold storage system was shipped from China for on-site assembly and commissioning, with technical support provided throughout the installation process.
01 Equipment Shipment
Refrigeration equipment and cold room materials were shipped from China to the African project site. The delivery covered components for three 15-ton blast freezers and two 200-ton frozen-storage rooms, including refrigeration units and insulated enclosure materials.
02 On-Site Installation
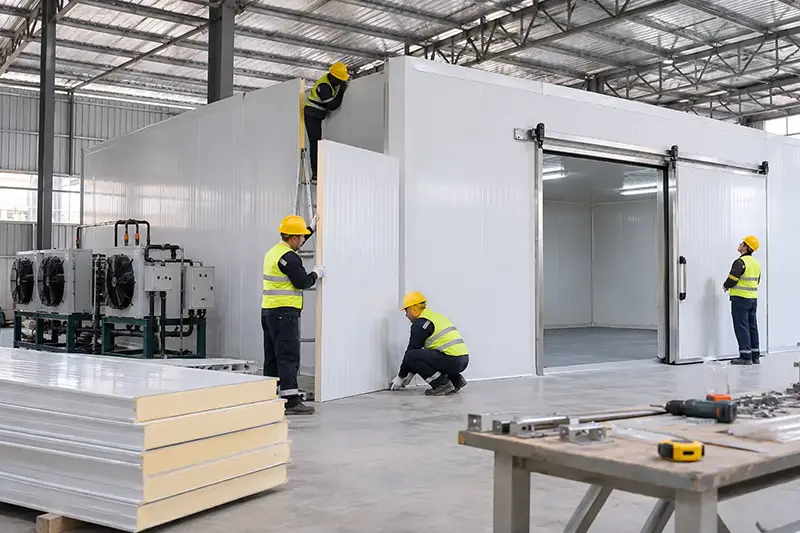
The five cold rooms were assembled at the poultry processing facility, with refrigeration equipment, insulated panels and heavy-duty sliding doors installed on-site. Detailed technical drawings and remote guidance from LINBLE supported the installation process.
03 Commissioning & Acceptance
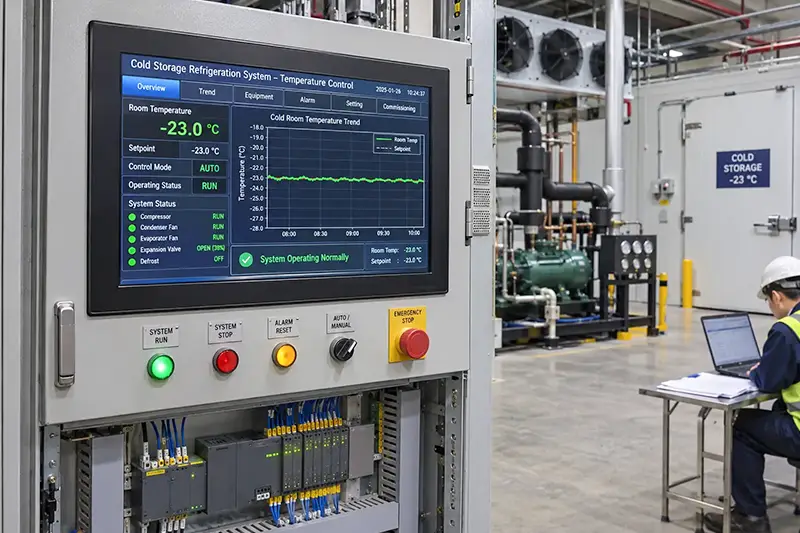
Following installation, the refrigeration system underwent on-site commissioning. According to the project records, the completed facility passed its first inspection by local agricultural and health authorities, allowing the plant to proceed toward full-scale operation.
Operating Results:
Reaching −18°C in 10.5 Hours Against a 12–18-Hour Target
Following commissioning, the project records reported a 10.5-hour freezing cycle to bring chicken core temperatures below −18°C, exceeding the original freezing-time target.
10.5 hours
Reported freezing cycle to bring chicken core temperatures below −18°C, against a 12–18-hour target.
≤1.2%
Reported product moisture loss, compared with 3.5% in the previous setup.
30,000–35,000
Chickens processed daily, according to the project records.
Freezing Performance & Product Quality
Performance Indicator | Original Target / Previous Condition | Reported Result |
Freezing Time | 12–18 hours | 10.5 hours |
Product Moisture Loss | 3.5% in the previous setup | ≤1.2% |
Daily Processing Performance
The facility reportedly supported daily processing of 30,000–35,000 chickens, with no significant product backlog or rewarming reported during the transfer between processing stages.
Customer Feedback & Further Cooperation
The customer recognized the value of LINBLE’s technical drawings and remote installation support. According to the project records, this cooperation continued into a second-phase cold storage project for poultry by-product processing.